What hole sizes, spacing and accuracy can a 3D CNC beam drilling machine hold?

What hole diameter range and plate thickness can the YM-3D1250 drill?
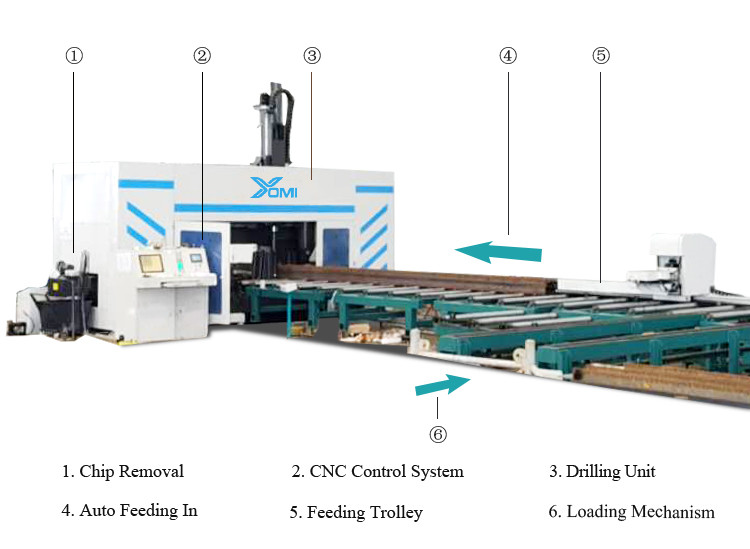
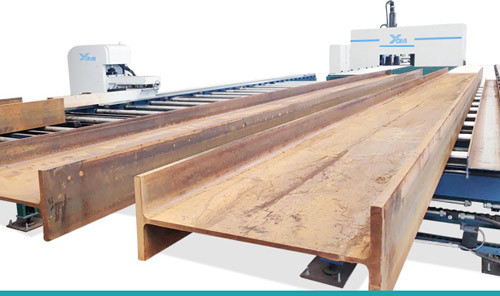
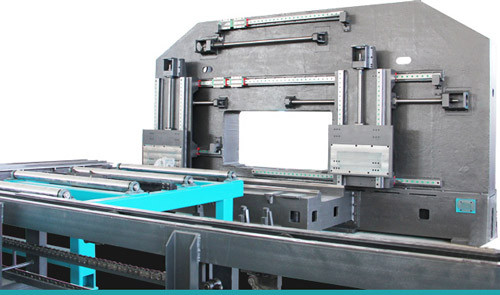
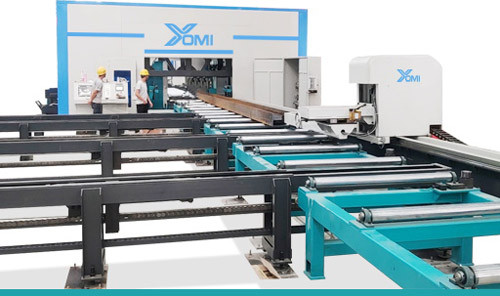
The YOMI YM-3D1250 drills holes from 8 mm to 40 mm diameter through material up to 80 mm thick. Three independent 15 kW drilling power heads work the web and both flanges in the same clamping pass, so a beam does not need to be flipped. The BT40 spindle (convertible to M4) runs at 30 to 3000 r/min and accepts carbide or HSS tooling. Workpiece width ranges from 200 to 1250 mm, covering H beams, U beams, box beams and angle steel.
How accurate is hole positioning on a 3D CNC beam drilling machine?
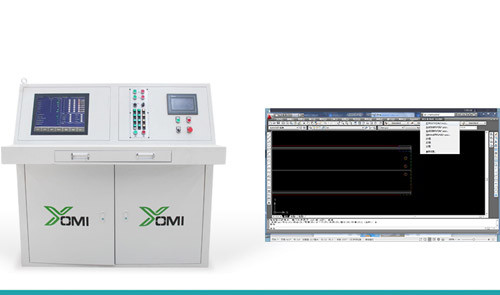
The YM-3D1250 holds hole-group accuracy within 0.5 mm inside a hole group under 640 mm, and 1.0 mm per 10,000 mm between hole groups. Because drilling is a cold process, there is no thermal distortion of the hole geometry the way plasma or flame cutting holes causes. CNC axes position the beam with servo feeding at up to 20 m/min on a 10 t capacity conveyor, and the machine reads TEKLA 3D DSTV files directly, so hole coordinates come from the model rather than manual layout.
What minimum hole spacing and edge distance should I design for?
Follow your connection design standard: AISC and EN 1090 both recommend a minimum edge distance of roughly 1.5 times the bolt diameter and minimum hole-to-hole spacing of about 2.5 to 3 times the hole diameter. The machine itself drills any spacing your DSTV file contains, but very tight clusters limit tool and clamp clearance, so check the actual drill diameter plus fixture clearance with the supplier before finalizing dense hole groups. Sending your densest real connection plate detail for a trial cut is the safest way to confirm.
Can a beam drill line make countersunk, counterbored or slotted holes?
The standard configuration produces round through holes from 8 to 40 mm. Because the spindle is a BT40 taper with 30 to 3000 r/min speed range, countersinking and counterboring are possible with special tooling, and short slotted holes can be produced by a programmed drill-and-step sequence. Long mill slots and shaped cut-outs are usually left to the cutting station. State your countersink, counterbore and slot requirements explicitly in the RFQ so the tooling list and quotation match your connection details.
What clearance hole sizes should I use for standard structural bolts?
For standard clearance holes, common practice under EN 1090 and AISC is: M12 bolt to 14 mm hole, M16 to 18 mm, M20 to 22 mm, M24 to 26 mm, M30 to 33 mm. Oversized holes add roughly 2 to 4 mm, and short or long slotted holes follow the dimension table in your design standard. The important thing is that your TEKLA or CAD model carries the correct hole size, because the YM-3D1250 drills exactly what the DSTV file specifies with no manual re-entry.
Why don't drilled holes line up during bolt assembly on site?
Mismatched bolt holes are rarely a drilling machine accuracy problem. The usual causes are: beams that were welded or straightened after drilling and twisted in the process, accumulated tolerance across multiple fitted parts, an outdated DSTV file that does not match the current model revision, or shipping and handling distortion. Drilling after welding and straightening, running a first-piece check against the drawing at the start of each job, and controlling model revisions eliminate almost all field fit-up problems.
How close to the beam end can holes be drilled, and what is the shortest workpiece?
The YM-3D1250 processes short material automatically from 3000 mm up to an effective feeding length of 12 m, and 12 or 15 m configurations are available. End distance follows your design standard, typically at least 1.5 times the bolt diameter, but very close to the physical beam end the clamping and support rollers need enough material for a stable grip. If your jobs include frequent short connection beams below 3 m, plan to run them as manual or offload work, or confirm the minimum length with the supplier at quotation stage.
Do drilled holes need reaming or deburring before galvanizing and bolting?
No reaming is needed. Mist cooling at 0.5 MPa with sharp carbide tooling produces a clean, cold-cut hole wall without the recast layer that thermal cutting leaves. A light deburr of the exit-side burr before hot-dip galvanizing is good practice so the zinc coating builds up evenly and bolts seat flush. Inspecting one hole group per beam with a go/no-go gauge keeps tool wear from creeping into production, since drill bits typically need regrinding after several hundred holes depending on material hardness.
Technical Specifications of 3D CNC Beam Drilling Machine
| Parameter | Value |
|---|---|
| Share | |
| Categories | 3D Beam Drilling Machine |
| Brand | YOMI CNC Cutting&Welding Machinery |
| Product Specifications | YM-3D1250 |
| Beam web height | 200-1250mm |
| Max drilling thickness | ≤80mm |
| Max drilling hole diameter | ¢40mm |
| Spindle motor power | 3x15KW |
| Effective feeding length | 12m |
| Maximum feeding speed | 20m/min |
| Positioning CNC axis moving speed | 10~6000mm/min |
| Feeding CNC axis moving speed | 10~12000mm/min |
| Model | YM-3D1250 |
| Workpiece | H beam, U beam, box beam, angle steel |
| Maximum workpiece width | 1250 mm |
| Drilling diameter | 8 to 40 mm |
| Spindle | BT40 taper, convertible to M4, 30 to 3000 r/min |
| Spindle motor power | 3 x 15 kW |
| CNC axes | 7 |
| Hole accuracy | 0.5 mm within a hole group under 640 mm; 1.0 mm per 10,000 mm between groups |
| Feeding | 10 t capacity at up to 20 m/min |
| Main host size and weight | About 5600 x 1600 x 3400 mm, about 20,000 kg |
| Item | Parameter |
| H beam | 150 x 80 to 1250 x 600 mm |
| U beam | 150 x 80 to 1250 x 400 mm |
| Box beam | 150 x 80 to 1250 x 400 mm |
| Angle steel | 200 x 200 x 16 mm |
| Thickness | 80 mm or less |
| Length | 12 or 15 m, or customized |
| Short material limit | Automatic processing from 3,000 mm |
| Drilling power boxes | 3 pcs |
| Drilling hole diameter | 8 to 40 mm |
| Spindle speed | 30 to 3000 r/min |
| Spindle taper hole | BT40, convertible to M4 |
| Spindle motor power | 3 x 15 kW |
| CNC axis quantity | 7 pcs |
| Fixed, moving and intermediate shaft servo power | 3 x 2 kW |
| Positioning CNC axis speed | 0 to 10 m/min |
| Feed CNC axis speed | 0 to 5 m/min |
| Machined hole accuracy | Adjacent holes in a group under 640 mm: 0.5 mm; adjacent hole group distance: 1.0 mm per 10,000 mm |
| Feeding trolley servo motor power | 5 kW |
| Maximum feeding speed | 20 m/min |
| Maximum feeding weight | 10 t at 1 t/m |
| Maximum width of workpiece | 1250 mm |
| Mist cooling nozzles | 3 pcs at 0.5 MPa compressed air |
| Main host dimension, L x W x H | About 5600 x 1600 x 3400 mm |
| Main host weight | About 20,000 kg |
| Item | Traditional radial drilling, YOMI YM-3D1250 |
| Layout and marking | Manual measuring and scribing, Automatic from the TEKLA DSTV model |
| Faces per setup | One face, re-clamped for each face, Three faces in one pass |
| Hole accuracy | Depends on operator skill, 0.5 mm within a hole group |
| Consistency | Varies by shift and operator, Program driven and repeatable |
| Throughput | Low, with multiple handling steps, Continuous roller-table flow at up to 20 m/min |
Product Gallery

Applications
The 3D CNC Beam Drilling Machine is widely applied in steel structure prefabricated buildings, bridge and infrastructure construction, shipbuilding and marine engineering, heavy machinery manufacturing, power plant and industrial facilities, and offshore wind power structures.
Learn more about the 3D CNC Beam Drilling Machine:
https://www.steelstructurer.com/pid18376284/3D-CNC-Beam-Drilling-Machine.htm
For more information about 3D CNC Beam Drilling Machine and other steel structure intelligent equipment, contact YOMI CNC Cutting & Welding Machinery. Our team of experts is ready to help you find the best solution for your manufacturing needs.

- Full Name:
- YOMI WhatsAPP
- Tel:
+86 19053498672
- Email:
- sales@yomi-china.com
- WhatsApp:
- 8619053498672
- Address:
- Factory Adress: 9 Changjie Road, Ningjin,Dezhou, P.R.China